Analytics header

Monday, June 26, 2023

To Data Model or not to Data Model

The ongoing debate about where and how MES fits in new era of digital technologies is raging. Its not surprising and in fact to be expected in any kind of change, basically the old guard vs the new guard. Of course you have to believe that the 4th industrial revolution is really a paradigm change. Something that I clearly align with and have some background to do so since I have been studying this phenomena since the 1990s.

As in other paradigm shifts there will always be a bit of the old that is part of the new. Steam power has not completely disappeared, it still relevant in specialized application but it is not the main source of energy powering industrial operations. This leads us to ISA-95 that I believe is a relic of the current "industry 3.0" era and not directly relevant in the new digital paradigm. (note I purposefully am trying to minimize the use of "Industry 4.0" since it starting to get a negative connotation with all the hype going on). But, that being said there are elements of ISA-95 and other best practices that may be relevant in the new paradigm, ie the old in the new?

If we let history be our teacher we can probably come up with some prediction and that is where the data model topic is interesting. ISA-95 includes a data model and all the established MOM solution include a data model that based on the available technologies at the time that seemed appropriate. The question is then; is the quest to achieve the nirvana of one standard monolithic data model for all manufacturing achievable and is it still relevant with the new digital technologies? The answer I think is clearly no and no, as far as I know there are very few, if any, examples of an organization achieving a real working standard data repository for all its operation and its not because of lack of trying.

The bottom line here is that striving for a single standard data model in a monolithic repository is a fools errand, regardless of if we try to implement it with modern digital technologies. That being said a common, shared and interpretable view of manufacturing operations is still needed and critical. In fact it's at the core of Industry 4.0, in that its the data and information that gives us the Visibility, Transparency, Predictive Capacity and Adaptability. This holistic view into the manufacturing operations is also at the core of the CIM concept from the 80s that advocated a common "shared knowledge" that all operational activities in plant uses in order to streamline to manufacturing of products. That means that both paradigms are aligned around the same challenge that to improve manufacturing operations we need to all have a common understanding and view into the operation!   

The CIM Enterprise Wheel (c)1993, SME.

The difference is how we achieve this common and shared view (information and knowledge). In the old paradigm it was the notion of a strict and rigidly structured data model, in the new paradigm we have relaxed these requirements to allow for analysis from both structured and unstructured data. I can hear the skeptics already; how can you gain any insights with different solution each having their own data structures? A few things to consider here: We do need context and this context should be defined at the source. We need to simplify data structures and get away from multiple levels of abstractions needed to run monolithic process driven solution.  Adhere to some simple shared guidelines using a consistent data dictionary that allows for flexibility within your organization. (I know this sounds overly simplistic and see part II of this blog post). With these principles we can adopt many of the modern digital tools to curate views into our data, on demand with the flexibility needed for common and personalized views and insights including of course AI.     

Let's take at an example where different solutions all represent some data about a lot of materials and its product code. The material can be referenced as Lot, Batch, Units, Pack, Kit, etc and the product code can be references as SKU, Item ID, Product, Material Number, etc. We of course immediately recognize these different names as similar because we understand how they are used. In the old paradigm we had to enforce strict rules in structure and semantics for software solution in order to visualize and analyze this data. That is however changing with new digital technologies and modern analytics platforms.  

It is also where AI can help, you see simply put AI is good at finding patterns. Its not that AI understands what the meaning of Item and Material Number is. It simply is looking for similarities in the relationship to other data structure and how its used to see that Item and Material Number really are very similar. With enough data volume and variety this can be easily detectable. Notice I said volume and variety this is where Cloud based system are important. Using isolated traditional monolithic system data sources will never get you to this point, even if they are lift and shifted to the cloud. You need a modern cloud native operational platforms that provides easy access to the their data that can be amassed and used to identifying these patterns.

I know there are a number of concepts discussed here and there may be some lack of depth in the discussion. I promised a follow up on this post with some more detail. But assuming this is true, just think about it. It means we can relax the strict data type and structure requirements and allow citizen developers to extend template data structures to create solution to solve operational problems and know that we can still gain valuable insights about operations, and again the more data we have to more insight we have. The conclusion here is: prioritize data volume and variety and not monolithic structures.

Sunday, June 11, 2023

4 Questions As a Guide Towards True Digital Transformation

Most people that have heard me talk about digital transformation are probably sick of hearing me talk about the "order of magnitude" productivity gain that is promised by the ongoing digital industrial revolution. But here again it is a key principle that can be used to understand transformation and navigate through the existing maze of confusion of what is and is not digital technology. Simply put digital technology is a technology that can directly impact industrial or manufacturing operations to bring about an order of magnitude productivity increase. 

I have compiled 4 critical elements that can help you sort through the maze of different technologies that are touted as digital, Industry 4.0 or Smart Manufacturing technologies based on this principle. These 4 elements can be framed as question that guide evaluation and selection of technologies:

Is it adopted and implemented in a "Bottom Up" manner?

Adoption and implementation are performed in an agile method, starting small in an iterative manner and building on outcome of each iteration. Agile approaches are an inherent part of the digital transformation and advocate a way to learn faster by short and rapid test-fail-learn cycles. The overall manufacturing systems solution is built from the bottom up in an iterative manner. 

This is in stark contrast to the traditional system approaches, including MES, where top down hierarchical processes are used to provide a solution that fits within specific constraints that is hard to change. There should be no "gap assessments", the technology is adapted to the process in contrast to fitting the process to the solution. It also removes the difficulties associated with adhering to complicated standards and systems. It frees engineers to focus on building solutions rapidly that fit the process and increases the rate of implementation by an order of magnitude (here I go again...). There are some interesting implications to this approach one of which is that Industry 3.0 standards such as ISA-95 becomes less relevant in this context.

Does it inherently support and enable Continuous Improvement?

Lean principles are still the most effective way to achieve productivity increases in an industrial operation and therefore the technology should be a tool to implement these operational improvements. The adoption of the technology should be done in a methodical PDCA or DMAIC cycle with each improvement supporting the next. Changes and modifications to a solution are easy and support iterative and constant improvement. The technology solutions are targeted at improvement areas with clear and quantified goals.   

It should be no surprise that regardless of the paradigm shift that is going on Lean and the principles of TPS are still real and valid. There is a close connection between the continuous improvement process and agile (bottom up) development approach of using the technology/solution. Th technology should be a Lean tool that allows engineers to rapidly iterate thru solutions to problem building digital content to an effective solution. 

Does it offer a Democratized approach and how does it enable "Citizen Developers"?

Users and implementors of the technology do not need to have unique and specific skills that are common for software, IT or automation engineers. Engineers and SMEs can rapidly adopt the technology to develop solution for the operations. The technology is so easy to use and learn that it is effectively accessible to most people with a basic level of technical aptitude. This allows the people that are closest to the process to craft solutions that are focused on solving a problem or provide an improvement. The technology should be adopted by people from within the operation rather than implemented by external parties.

Democratization and the citizen developer is an important aspect of the digital transformation. With modern digital technology we all can become builders of digital content. We already do this when using office tools such as Word and Excel and now we can even easily program our IoT door to open automatically when we get within range so we don’t have to take our key out. This is a big change compared to the high level of skills and expertise needed to build even simple automation tasks in traditional systems. No-Code/Low-Code is a key enabler of Democratization, it allows people with no programming or IT skills to build content that automates manufacturing processes in a simple and intuitive way. 

I find that for bigger organizations citizen development may be alarming, i.e. they feel it is akin to "arming the rebels". However there is no way around it, the benefits far outweigh the risks in this case and democratization of technology is key element of the new digital age. At the same time most of the new platform technologies provide accessible and transparent control and management of content being created and consumed. 

Is the technology able to provide Human Centric solutions?

The use of the technology should result in solution that serve humans or specifically frontline operators. It has to be intuitive, simple, easy to understand and easy to use. It has to serve the frontline operator by making him more productive, the operator is the key to the productivity gains promised by digital technologies in I4.0  

Modern digital technologies and tools are built on the principle of supporting human activity, that is what makes them so effective and so widely adopted. People are the key to unlocking productivity gains from digital technologies, that therefore have to focus on supporting human activity. The premise is that in order to increase productivity technology needs to support the human operator. In the new digital age manufacturing needs to enable the connected worker whose tasks are monitored and supported by a larger network of digital tools. In addition the technology should be used to capture additional digital data streams such as instrumentation of the human activity, the data that human operators collect, input they can provide about the process, and more. 

In conclusion, if a technology is not able to impact your operations in this significant way then its not digital technology - simply drop it from the list. Let's take a simple example: SaaS MES that is purportedly in the cloud and requires experts with specific skills set to configure and use with a 6+ months implementation time frame. This is not and example of digital technology. You should be seeing quantifiable productivity increase results within weeks of adopting any technology.  Another example is if the technology implementation requires a waterfall/phased method that requires design of the substantial parts of the solution upfront then it is not a digital technology!  

You can watch me talk about these topics on the Manufacturing IT Podcast with Daniel Langley.

Maybe this will also nudge the skeptics out there since speed, effort and real world double and triple productivity gains are becoming real and undeniable. Charlie Chaplin once said "if you look down, you will not see the rainbow".

Sunday, May 28, 2023

The Genius of the Toyota Production System Explained

So much has been written about the Toyota Production System (TPS) that you may be wondering why in this day and age were the focus of most of this blog is on digitalization and Industry 4.0, I am bringing this topic back up? It should be no surprise that regardless of the paradigm shift that is going on Lean and the principles of TPS are still real and valid. The reason is that under all the tactical concepts that we in general refer to as "Lean Manufacturing" it addresses a basic characteristic of all manufacturing systems and that is that they are inherently chaotic! In fact they are a special type of chaotic system called Complex Adaptive System or CAS, a topic that I believe is critically important to understand in these transformational times.

McElroy, Mark. (2000). Integrating Complexity Theory, Knowledge Management, and Organizational Learning. Journal of Knowledge Management. 

Before explaining what Chaos and CAS are and why I believe this to be true, I wanted to state the conclusion. The genius of TPS is that the concepts and strategies that it employees are directly built to use the characteristics of the CAS to its advantage, ie to increase value and productivity. The two fundamental concepts that are central to Lean and TPS that back this hypothesis are:
  • Understanding that adaptability to change is critical. Lean provides for effective management small deviation and big changes with a focused and controlled manner with strong discipline, clear objectives and effective execution. Examples are Andons, Kaizen, Gemba, Hoshin Kanri, Poke Yoke, etc. that are designed to provide an effective way to deal with the repeatable patterns (good or bad) within the system.
  • Understanding the boundaries between chaotic dynamics and order. Lean strives to coral the unpredictable nature of CAS by making a discrete non linear system more linear. Reducing batch size, making value flow, JIT, Heijunka, Kanban, SMED, etc. makes the system more continuous and less discrete and therefore more predictable.
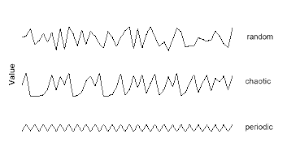
In order to better understand this premise, I really need to provide a primer about Chaos and Complex Adaptive Systems. First a disclaimer - this is a diverse and complex topic and the following explanation is very high level and simplistic. Chaos sometimes is confused with randomness, however it is different. Here is a simple comparison:


Random

Chaotic

Periodic

Unpredictable Path

Unpredictable Pattern

Unpredictable Path

Predictable Pattern

Predictable Path

Predictable Pattern


This means that systems that exhibit chaotic behavior are impossible to predict but they have predictable patterns that repeat. On a side note; we as humans are very good at identifying patterns, which means we are inherently very good at operating in chaos. That is also what AI is good at and why its application in manufacturing context is so interesting and offers so much potential. 

As mentioned a CAS is a special type of chaotic system that exhibit chaotic dynamics and emergent behavior and includes of course our favorite system the manufacturing organization. Other examples of CAS are weather, traffic, ant colonies, the stock market, social and organizations. A CAS behaves and evolves according to three key principles:
  • Order and control is emergent. The overall behavior of the system of elements is not predicted by the behavior of the individual elements. There is a natural transition between equilibrium points through environmental adaptation and self-organization.
  • The system's history is irreversible or irreducible. Irreversible process transformations cannot be reduced back to its original state. They evolve and their past is co-responsible for their present behavior.
  • The system's future is often unpredictable. Non linear and therefore not predictable but yet have repeatable identifiable pattern. Predetermined patterns within their complexity describe potential evolutions of the system. 
OK, now with this information we can reflect on what this means in the context of Lean and TPS. Jim Womack famously defined the 5 principle of Lean as a result of studying TPS and how it works. By looking at how each of these principles is directly designed to use the characteristic of a CAS the genius of TPS is revealed.
 
Lean Thinking (1996), James P. Womack and Daniel T. Jones
  • Identify Value: This is in fact not directly related to the manufacturing being a CAS, it is really just a sound business principles. I.e. make sure to have clear objectives and know what to focus on- similar to Deming's "consistency of purpose". Identifying the value stream provides the framework for prioritization of how and where to optimize.
  • Map the Value Stream: Understanding the value creation process and the details in the value stream helps in understanding the specific key attributes that impact the behavior of the system. In a CAS there are dependencies between key attributes and specific patterns that indicate either good or bad behaviors. This is to understand what in the value stream may trigger unwanted states, ie.e the famous "butterfly effect". For example the rectangles drawn on the weather forecast indicating that a Tornado is likely.   
  • Create Flow: Make sure that the production value stream flows since systems that flow are continuous and more linear in contrast to nature of discrete "stop and go" type of behavior. Reducing the unit size (one piece flow) eases flow, with the smaller the unit the better. Without consistent flow the system becomes more non-linear and may exhibit catastrophic patterns. For example getting stuck behind the guy who can't out of the way when boarding a plane (exemplified by Mythbusters). 
  • Establish Pull: Consistent flow can be nearly guaranteed if you pull rather than push the elements of the system. It secures blockages are identified immediately and removed, simply because you can't pull with something in the way. Think what happens when you are behind two trucks overtaking on a highway causing traffic to backup.  
  • Seek Perfection: This principle is to ensure that we can keep the CAS in states that we can predict. By striving to keep the manufacturing system as close as possible to linear (consistent flow) we can predict and guarantee performance and behavior. However it also provide tools to identify unwanted patterns and ways to quickly address states that are undesirable.     
Toyota has always advocated a cautious approach to new technology and that is a a problem. The n-1  approach to technology advocated by Lean (the use of proven technology, not the latest and greatest) is sometimes used as an excuse to maintain status quo. In these times of change with all the new digital technology available this seemingly puts Lean companies at a disadvantage. However if you approach these technologies as a way to Lean, to reduce waste, to create flow and execute pull then the value of the technology can easily outweigh the risk. In addition the n-1 concept was really meant for production equipment, i.e. to not increase the risk of interrupting the production flow and quality issues.

Its important to understand how digital technology can be used to support a Lean system. Remember the new paradigm offers an order of magnitude productivity increase and herein lies key motivator. Digital transformation needs to support a lean system, it has provide additional tools in the Lean toolbox. Digital technology can be catalyst to a Lean organization where continuous improvement happens faster and more effectively and that is how the "order of magnitude increase" is realized.

So the genius of TPS is simply put that Toyoda understood behavioral dynamics of his manufacturing operation even without knowing its a CAS and was able to put together a management strategy to directly impact the characteristics of the system with optimization in mind. When operational principles are nicely aligned with the science behind it there its not a surprise that its successful. We should now do the same to transform lean operations with digital tools so that we can hit the digital transformation jackpot. 


Saturday, May 20, 2023

How Electricity Goes Around the Bend & Where is the Electricity Manager?

The Ghost Town

I recently was on a motorcycle ride to Bodie, a gold rush ghost town in California that is now a state park. I was fortunate enough to be with Mark, who apart from running motorcycle adventure rides, who is also is a bit of a gold rush history buff. He told a story about how electricity was perceived during the boom days at Bodie.

Electricity first came to the gold rush mining towns in the California desert of the Eastern Sierras in the 1890s and it was, as you would expect, quite a spectacle. It brought with it a major change in the way gold was mined and processed and offered great productivity increases.  At the the time there was a common misconception that the electricity power lines had to be run straight because the electricity would shoot out if it there was a bend in the line. Basically it could not flow around a bent or wire that changes direction.  Here is a bit more background from Chat GPT: "Did people believe that electricity can't flow through a bent wire in the gold rush towns?"

"One popular misconception of the time was that electricity followed the path of least resistance. In this context, the notion that electricity could not flow through a bent wire might have arisen. People might have believed that the bent shape of the wire created a higher resistance, hindering the flow of electricity."

Considering that this was a new technology that was brought to remote towns where the living, to say the least, was hard and dangerous such a misconception seems reasonable. Yet we can draw some striking similarities with this scenario and the introduction of digital technologies to manufacturing plants. Manufacturing plants are operational islands where financial survival is always a top priority and digital technology is not fully understood, or maybe understanding it is not the most important priority. Like electricity in the gold rush town, its hard to relate to a new technology that has lofty and even ungrounded promises such as "a fundamental change to how we live and operate" and "an order of magnitude productivity increase".

Managing Electricity

During the 2nd industrial revolution, where we transformed from steam to electricity all plants had an "Electricity Manager". Again Chat-GPT for some wisdom: "what was the role of the electricity manager during the 2nd industrial revolution?"

"Overall, the role of an electricity manager during the Second Industrial Revolution involved overseeing the generation, distribution, and management of electricity. Their responsibilities encompassed technical, safety, operational, and financial aspects to ensure the reliable and efficient supply of electrical power to support industrial and societal advancements during this transformative period."

So clearly we do not have this role in our manufacturing plants today, we simply pay for electricity as a service. Does this sounds eerily similar to the current roles of CIO or CDO in managing digital technology? What is the destiny of IT organization and CIOs? Will XaaS (Anything as a Service) become common place and make IT redundant?

Oh the Skepticism

I tell these stories to most skeptics that I meet in an attempt to explain that a new paradigm requires new thinking. We will not be able to experience productivity increases until we realize that what we have at our hands is so different than anything we have seen before. In other words electricity does flow around bent wires, data is safe in the cloud, citizen developers can build complex systems, you can validate a solution in hours, control of democratized technology is easy, IIoT can be safe, it's also for all size companies, etc. Oh and one more that is quite controversial; MES, LIMS, WMS, etc. are not digital technologies - they are relics of the previous industrial age (industry 3.0). They are what steam was to electricity!

The challenge that I face on a daily basis is how to dispel the myths of digital technology and relieve the skepticism that is inherent in most manufacturing organizations? This is in the perspective of the bigger challenge that is how do we plan to transform industry so they can start capitalizing at the order of magnitude productivity gains. In the words of Søren Kierkegaard: "Life can only be understood backwards; but it must be lived forwards."